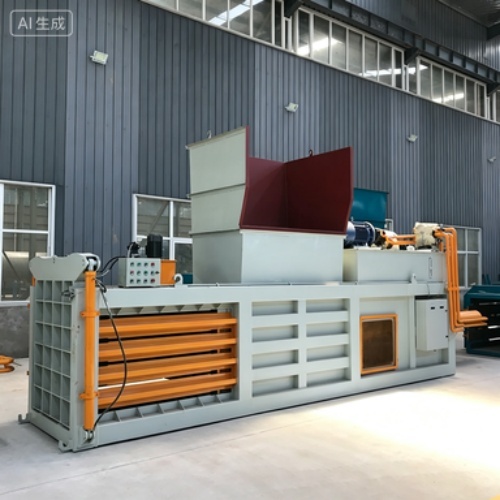
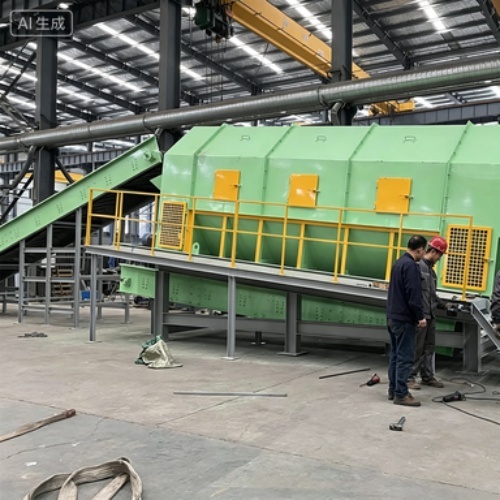
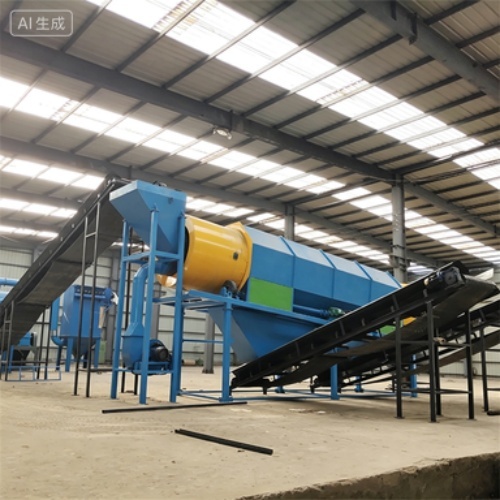
Heavy Duty Industrial Trash Shred Pack Sort System
Description
Industrial Waste Shredder Baler Sorting Line Commercial Rubble Granulator Compactor Unit Metal Scrap Shear Bale Forming Device: The Ultimate Solution for Heavy Duty Trash Crusher Packing System Solid Waste Reduction Bale Press Machine Recyclable Material Separation Shred Line
In the modern landscape of waste management and resource recovery, efficiency is not merely a luxury but a necessity. Our advanced Automated Refuse Processing Conveyor Belt Municipal Garbage Crushing Balancing Plant Plastic Film Shredder Compression Wrapper represents the pinnacle of engineering designed to transform chaotic waste streams into manageable, high-value commodities. This comprehensive system integrates multiple stages of processing, from initial size reduction to final baling, ensuring that businesses can handle diverse types of refuse with unprecedented speed and precision. By adopting this state-of-the-art technology, organizations can significantly reduce disposal costs, minimize environmental impact, and enhance their sustainability profiles through effective material separation and volume reduction.
The core of this solution lies in its modular design, which allows for customization based on specific operational needs. Whether dealing with bulky municipal garbage, dense metal scrap, or delicate plastic films, the machinery adapts seamlessly to the task at hand. The integration of heavy-duty components ensures durability and longevity, even under the most demanding conditions. This robust construction means less downtime and lower maintenance costs over the lifecycle of the equipment, providing a superior return on investment for industrial clients worldwide. Furthermore, the automated nature of the system reduces labor intensity and improves workplace safety by minimizing direct human interaction with hazardous materials.
Key Features
High-Efficiency Size Reduction Technology: Utilizing advanced shredding mechanisms, the system breaks down large volumes of waste into uniform sizes, facilitating easier handling and further processing. This feature is crucial for optimizing the performance of subsequent baling and compression stages.
Automated Material Separation: Equipped with sophisticated sorting algorithms and mechanical separators, the line effectively isolates recyclable materials from non-recyclables. This capability enhances the purity of recovered resources, making them more attractive to recycling markets and increasing revenue potential.
Versatile Baling Capabilities: The bale forming device supports various density settings and bale sizes, accommodating different types of materials such as paper, cardboard, plastics, and metals. This flexibility allows operators to tailor output specifications to meet specific customer requirements or logistical constraints.
Robust Construction and Durability: Built with high-grade steel and reinforced components, the machinery withstands continuous operation without compromising performance. This resilience ensures consistent output quality and extends the service life of the equipment.
User-Friendly Control Interface: An intuitive control panel enables operators to monitor and adjust machine parameters in real-time. This feature simplifies operation, reduces training time, and enhances overall productivity by allowing quick responses to changing waste characteristics.
Detailed Description
The Industrial Waste Shredder Baler Sorting Line is engineered to address the complex challenges associated with modern waste management. At the heart of the system is a powerful shredder capable of processing a wide range of materials, including organic matter, plastics, metals, and mixed refuse. The shredding process is designed to maximize surface area exposure, which aids in subsequent separation and compression steps. Following shredding, the material moves along an automated conveyor belt system, where it undergoes rigorous sorting. Magnetic separators remove ferrous metals, while optical sorters identify and separate various polymer types based on their spectral signatures.
Once sorted, the materials are directed to specialized balers or compactors. For instance, lightweight materials like plastic films and textiles are fed into a compression wrapper that forms tight, uniform bales suitable for storage and transport. Meanwhile, heavier materials such as metal scrap are processed through a shear mechanism that cuts and compacts them into dense blocks, optimizing space utilization during shipping. The entire process is monitored by a central control unit that adjusts speeds, pressures, and other variables to ensure optimal performance.
This system also incorporates dust suppression and noise reduction technologies, addressing common concerns associated with waste processing facilities. Enclosed chambers and filtration systems prevent the release of particulate matter into the environment, while sound-dampening materials reduce operational noise levels. These features contribute to a cleaner, safer working environment and help facilities comply with stringent environmental regulations.
Usage Scenarios
Municipal Waste Management Facilities: Cities and municipalities can utilize this system to process household waste, reducing the volume sent to landfills and recovering valuable recyclables. The ability to handle mixed waste streams makes it ideal for areas with limited sorting infrastructure.
Manufacturing Plants: Industrial facilities generating significant amounts of packaging waste, off-cuts, and defective products can benefit from on-site processing. By converting waste into bales, companies can reduce disposal fees and generate additional income by selling recovered materials.
Recycling Centers: Recycling operations can enhance their throughput and material purity by integrating this sorting and baling line. The precise separation capabilities ensure that recovered materials meet industry standards, opening up new market opportunities.
Agricultural Operations: Farms producing large volumes of plastic mulch, silage wrap, and other agricultural waste can use this system to manage their refuse efficiently. The compacted bales are easier to store and transport, reducing clutter and improving farm hygiene.
Construction and Demolition Sites: Builders and demolition contractors often face challenges in managing rubble and debris. This system offers a solution by crushing and compacting these materials, facilitating easier removal and potential reuse of crushed aggregates.
User Testimonials
After implementing the Industrial Waste Shredder Baler Sorting Line, our facility has seen a forty percent reduction in waste disposal costs. The automated sorting feature has significantly improved the quality of our recycled materials, leading to higher prices from buyers. The machine operates smoothly with minimal supervision, allowing our team to focus on other critical tasks. We highly recommend this solution for any organization looking to enhance its waste management practices.
We have been using the Heavy Duty Trash Crusher Packing System for six months now, and the results are impressive. The durability of the equipment is evident, with no signs of wear despite continuous operation. The versatility of the system allows us to process different types of waste without major adjustments, saving time and effort. It has become an indispensable part of our recycling operations.
The ease of use and reliability of the Automated Refuse Processing Conveyor Belt Municipal Garbage Crushing Balancing Plant Plastic Film Shredder Compression Wrapper have exceeded our expectations. The control interface is intuitive, and the technical support team has been responsive and helpful. Since installation, we have achieved a substantial increase in processing capacity, enabling us to handle larger volumes of waste efficiently.
Frequently Asked Questions
What types of waste can this system process?
The system is designed to handle a wide variety of waste materials, including municipal solid waste, industrial scrap, plastics, metals, paper, cardboard, and agricultural residues. Its modular design allows for customization to suit specific waste streams.
How does the system ensure material separation accuracy?
The system employs a combination of mechanical separators, magnetic drums, and optical sorters to achieve high-purity separation. These technologies work together to isolate different material types based on physical and chemical properties.
Is regular maintenance required?
Like all industrial machinery, regular maintenance is necessary to ensure optimal performance. However, the system is built with durable components and includes self-diagnostic features that alert operators to potential issues before they become serious problems.
Can the system be integrated with existing waste management infrastructure?
Yes, the system is designed for easy integration with existing conveyors, balers, and sorting equipment. Customization options are available to ensure compatibility with your current setup.
What safety features are included?
The system incorporates multiple safety features, including emergency stop buttons, protective guards, and interlock systems. These features ensure operator safety and compliance with international safety standards.
How does the system contribute to sustainability?
By maximizing material recovery and reducing waste volume, the system helps minimize landfill usage and conserve natural resources. The recovered materials can be reused in manufacturing processes, supporting a circular economy approach.
What is the expected lifespan of the equipment?
With proper maintenance and operation, the equipment is designed to last for many years. The use of high-quality materials and robust construction ensures long-term reliability and performance.
Does the system offer remote monitoring capabilities?
Yes, the system can be equipped with remote monitoring software, allowing operators to track performance metrics and receive alerts from anywhere. This feature enhances operational efficiency and facilitates proactive maintenance.
How does the system handle hazardous materials?
While primarily designed for general waste, the system can be customized to handle certain types of hazardous materials with appropriate safety measures and containment protocols. Consultation with our engineering team is recommended for specific applications.
What kind of support is provided after purchase?
We offer comprehensive after-sales support, including installation assistance, operator training, spare parts supply, and technical troubleshooting. Our global network of service providers ensures timely support regardless of location.


You may also like


${currentPro.title}