Deep Advanced RO Technology For Water Purification
Description
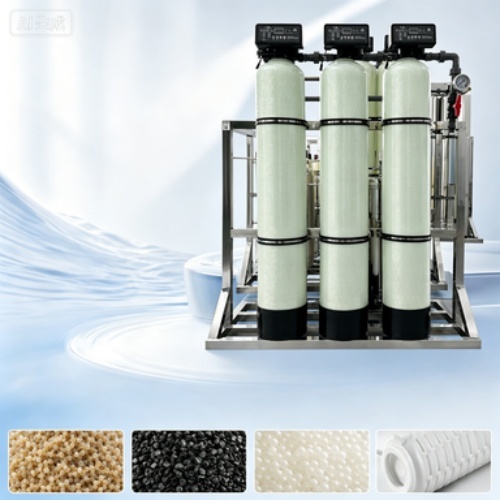
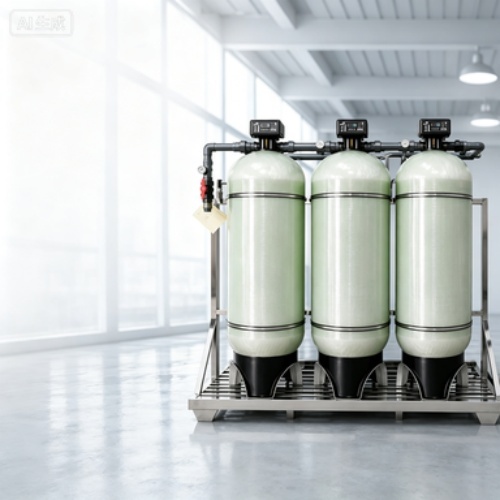
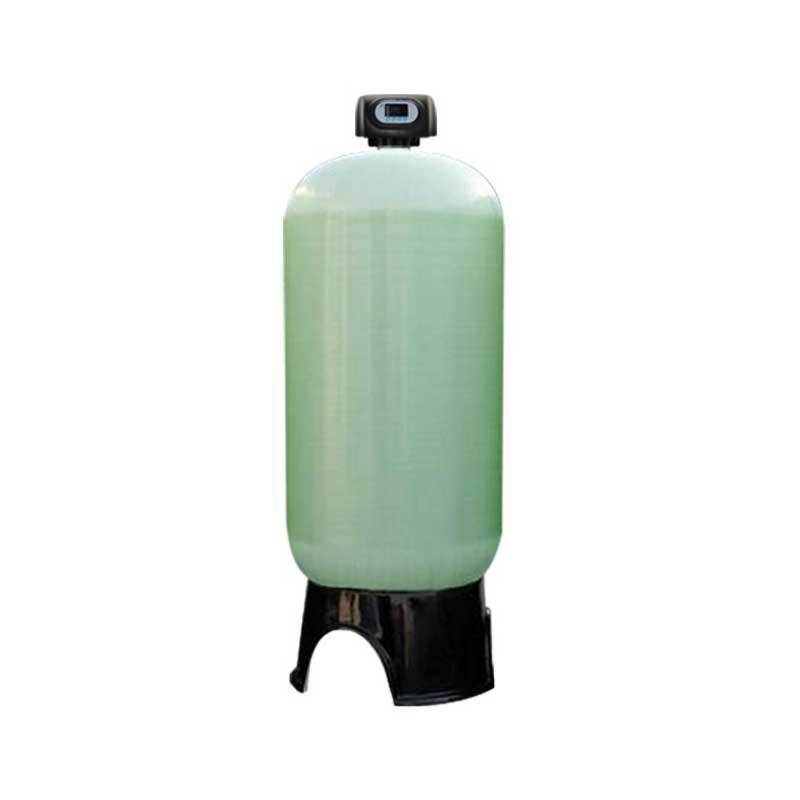
Industrial Waste Disposal Equipment Heavy Duty Industrial Water Treatment Commercial RO Water Filtration Plant Large Scale Water Softening System Advanced Waste Disposal Machinery High Capacity Water Softener System Reverse Osmosis Purification Unit Industrial Grade Reverse Osmosis Filter Large Volume Water Purification Equipment Overview of Advanced Industrial Water Solutions In the modern industrial landscape, maintaining stringent environmental standards and ensuring operational efficiency are paramount. The integration of high-performance waste disposal equipment and sophisticated water treatment systems has become a critical component for manufacturing facilities, commercial enterprises, and large-scale industrial operations. This comprehensive suite of solutions is designed to address the complex challenges associated with wastewater management, purification, and resource recovery. By leveraging cutting-edge technology in reverse osmosis purification and advanced filtration processes, businesses can significantly reduce their environmental footprint while optimizing water usage. The focus here is on delivering robust, durable, and highly efficient systems that meet the rigorous demands of heavy-duty industrial applications. These systems not only comply with global regulatory requirements but also provide long-term cost savings through improved water quality and reduced waste output. Whether dealing with chemical processing, food and beverage production, or pharmaceutical manufacturing, the ability to effectively manage industrial effluent and produce high-purity water is essential for sustainable growth and operational excellence. Key Features of the System The core strength of this industrial-grade solution lies in its modular design and superior engineering capabilities. The heavy-duty construction ensures longevity even under harsh operating conditions, making it suitable for continuous operation in demanding environments. A standout feature is the advanced reverse osmosis purification unit, which utilizes multi-stage membrane technology to remove impurities at a molecular level. This process is complemented by an industrial grade reverse osmosis filter that enhances the overall efficiency of the purification cycle. The system incorporates a large scale water softening system that effectively reduces hardness ions, preventing scaling in pipes and machinery, thereby extending the lifespan of downstream equipment. Additionally, the high capacity water softener system is engineered to handle fluctuating flow rates without compromising performance. The waste disposal machinery component is designed for maximum throughput, allowing for the rapid and safe processing of solid and liquid waste streams. Integrated automated controls provide real-time monitoring and adjustment, ensuring optimal performance and minimizing manual intervention. These features collectively contribute to a reliable, efficient, and environmentally responsible water management strategy. Detailed Description of Technology and Performance At the heart of this product line is the commercial RO water filtration plant, which represents the pinnacle of water purification technology. Utilizing semi-permeable membranes with precise pore sizes, this plant effectively removes dissolved salts, organic compounds, bacteria, and viruses from raw water sources. The industrial waste disposal equipment works in tandem with the filtration system to ensure that all byproducts are managed safely and efficiently. The large volume water purification equipment is capable of processing thousands of gallons per hour, making it ideal for facilities with high water consumption needs. The advanced waste disposal machinery employs thermal and mechanical processes to reduce the volume of waste, facilitating easier transportation and disposal in accordance with environmental regulations. The industrial grade reverse osmosis filter is constructed from corrosion-resistant materials, ensuring durability and consistent performance over time. Furthermore, the system includes pre-treatment stages such as sediment filtration and carbon adsorption to protect the delicate RO membranes from fouling and damage. This multi-layered approach guarantees that the final output water meets the highest purity standards required for industrial processes, cooling towers, boilers, and cleaning operations. The integration of these technologies creates a seamless workflow from raw water intake to purified water output and waste discharge, providing a holistic solution to industrial water challenges. Application Scenarios and Use Cases These versatile systems are applicable across a wide range of industries where water quality and waste management are critical. In the power generation sector, the large scale water softening system is used to prepare boiler feedwater, preventing corrosion and scaling in turbines and heat exchangers. For the pharmaceutical industry, the reverse osmosis purification unit provides ultra-pure water necessary for drug formulation and laboratory testing, ensuring compliance with strict hygiene standards. In the food and beverage manufacturing sector, the commercial RO water filtration plant is employed to treat process water, enhancing product taste and safety while reducing the use of chemicals. Mining and metallurgical operations benefit from the heavy duty industrial water treatment capabilities, which allow for the recycling of process water and the safe disposal of toxic sludge. Textile and dyeing industries utilize the advanced waste disposal machinery to treat colored wastewater, removing dyes and harmful chemicals before discharge. Additionally, semiconductor manufacturing plants rely on the high capacity water softener system to produce ultrapure water for wafer fabrication, where even trace contaminants can cause significant defects. The adaptability of these systems makes them suitable for both new installations and upgrades to existing infrastructure, providing a future-proof solution for water management needs. User Feedback and Testimonials Operators who have implemented these industrial water treatment solutions report significant improvements in operational efficiency and regulatory compliance. Many users highlight the ease of maintenance and the reliability of the heavy duty industrial water treatment components, noting that downtime has been minimized due to the robust design. Customers appreciate the clarity of the automated control systems, which provide intuitive monitoring of water quality parameters and waste levels. Several testimonials mention the substantial reduction in water procurement costs thanks to the effective recycling capabilities of the large volume water purification equipment. Users also praise the compact footprint of the advanced waste disposal machinery, which allows for easy integration into existing facility layouts. The performance of the industrial grade reverse osmosis filter has been particularly noted for its consistency, maintaining high rejection rates even during peak load periods. Overall, feedback indicates a high level of satisfaction with the total cost of ownership, citing energy efficiency and low maintenance requirements as key benefits. These positive experiences underscore the value proposition of investing in high-quality industrial water and waste management solutions. Frequently Asked Questions What is the expected lifespan of the reverse osmosis membranes? The membranes typically last between three to five years depending on the quality of the feed water and the effectiveness of the pre-treatment system. Regular cleaning and proper maintenance can extend their service life. Can this system handle high concentrations of salt or contaminants? Yes, the industrial grade reverse osmosis filter and the commercial RO water filtration plant are designed to handle varying levels of salinity and contamination. Custom configurations can be developed for specific high-strength waste streams. How much space does the large scale water softening system require? The footprint varies based on the capacity required, but the modular design allows for flexible installation options. Compact units are available for facilities with limited space, while larger systems can be configured for centralized water treatment plants. Is the waste disposal machinery compliant with international environmental standards? Absolutely. The advanced waste disposal machinery is engineered to meet or exceed international environmental regulations regarding waste discharge and handling. Documentation and certification support are provided to assist with compliance audits. Does the system require specialized personnel for operation? The system is equipped with user-friendly automated controls that simplify operation. While basic technical knowledge is beneficial, extensive training is not required for day-to-day functioning. Support services are available for more complex troubleshooting. Why choose this industrial waste disposal equipment over competitors? Our equipment stands out due to its combination of heavy-duty construction, advanced purification technology, and comprehensive waste management capabilities. The focus on durability, efficiency, and ease of use ensures a superior return on investment compared to standard market offerings. Conclusion Investing in top-tier industrial water treatment and waste disposal solutions is a strategic move towards sustainability and operational resilience. The products described herein offer a complete package for managing water resources and waste outputs in industrial settings. From the initial filtration stages to the final purification and waste processing, every component is designed to work harmoniously to deliver optimal results. By adopting these advanced systems, businesses can not only meet regulatory obligations but also enhance their brand reputation as environmentally responsible entities. The versatility and robustness of the heavy duty industrial water treatment and commercial RO water filtration plant make them indispensable assets for any serious industrial operation. Embrace the future of water management with these innovative and reliable solutions.


You may also like


${currentPro.title}